
Introduction
Hydraulic cylinder failure represents one of the most costly maintenance issues facing construction equipment operators, mobile hydraulics manufacturers, and industrial machinery plants. Premature seal wear, fluid leakage, and system downtime often trace back to a single root cause: improper bore finishing during cylinder manufacturing or rebuild.
Hydraulic cylinder honing is the precision finishing process that creates the ideal internal surface for hydraulic seals to function reliably under extreme pressures and continuous cycling. Unlike conventional boring or grinding, honing produces the specific surface texture, dimensional accuracy, and geometric precision that hydraulic systems demand.
When executed with proper parameters, honing extends seal life by 3-5 times, virtually eliminates leakage, and ensures consistent system performance over hundreds of thousands of cycles. Poor honing—or skipping this critical step entirely—leads to accelerated seal degradation, system contamination, and costly equipment downtime.
This comprehensive guide examines the technical requirements, process parameters, and equipment considerations for achieving optimal hydraulic cylinder bore finishing. Whether you’re a cylinder manufacturer producing thousands of units annually or a repair shop reconditioning construction equipment cylinders, understanding these principles ensures reliable, long-lasting results.
For broader context on honing technology across applications, see our complete guide to honing machines and manufacturing technology.
Why Hydraulic Cylinder Honing is Critical for System Performance
The Function of Surface Texture in Hydraulic Systems
Hydraulic cylinders operate under extreme conditions that demand precise bore finishing. Pressures ranging from 3,000 PSI in mobile equipment to 10,000+ PSI in industrial presses place enormous stress on seal interfaces. The cylinder bore surface directly impacts seal performance through three critical mechanisms:
Oil Retention and Lubrication: The crosshatch pattern created during honing forms microscopic valleys that retain hydraulic fluid. This oil film lubricates the seal during piston movement, preventing metal-to-metal contact and reducing friction. Without proper texture, seals run dry and fail rapidly.
Seal Seating and Conformance: Hydraulic seals must conform to the cylinder bore to create an effective pressure barrier. Surface roughness that’s too coarse prevents complete seating, allowing fluid bypass. Surface finish that’s too smooth provides insufficient texture for seal material to grip, again causing leakage.
Heat Dissipation: Friction generates heat at the seal interface. The honed surface texture facilitates fluid circulation that carries heat away from the seal zone. Poor surface finish concentrates heat, accelerating seal material degradation.
Economic Impact of Proper Honing
The investment in proper hydraulic cylinder honing delivers measurable returns:
- Extended seal life: 3-5x longer service intervals between seal replacement
- Reduced downtime: Fewer unplanned failures and maintenance events
- Lower fluid consumption: Elimination of leakage reduces hydraulic fluid costs
- System efficiency: Reduced internal friction improves hydraulic system performance
- Warranty protection: Many seal manufacturers require proper bore finish for warranty coverage
A construction equipment manufacturer processing 500 cylinders monthly reported 60% reduction in warranty claims after implementing precision honing with verified surface finish specifications. The ROI on their CNC honing equipment investment was achieved within 18 months through reduced rework and warranty costs alone.
Understanding Hydraulic Cylinder Surface Finish Requirements
Ra Value Specifications by Application
Surface roughness for hydraulic cylinders is measured using Ra (Roughness Average), expressed in micrometers (μm) or microinches (μin). The optimal Ra value depends on operating pressure, seal type, and application:
Standard Industrial Hydraulics (1,000-3,000 PSI)
- Ra specification: 0.2-0.4 μm (8-16 μin)
- Typical applications: Industrial presses, material handling, machine tools
- Seal types: Polyurethane, nitrile rubber (NBR)
- Crosshatch angle: 45° ±3°
High-Pressure Mobile Hydraulics (3,000-5,000 PSI)
- Ra specification: 0.15-0.30 μm (6-12 μin)
- Typical applications: Excavators, loaders, agricultural equipment
- Seal types: Polyurethane, PTFE composite
- Crosshatch angle: 40-50°
Ultra-High-Pressure Systems (5,000-10,000+ PSI)
- Ra specification: 0.10-0.20 μm (4-8 μin)
- Typical applications: Injection molding, metal forming presses, test equipment
- Seal types: PTFE, filled PTFE, polyimide
- Crosshatch angle: 35-45°
Construction Equipment (Variable Pressure)
- Ra specification: 0.25-0.40 μm (10-16 μin)
- Typical applications: Cylinders, stabilizers, steering cylinders
- Seal types: Polyurethane (primary), NBR (secondary)
- Crosshatch angle: 45° ±5°
Chrome-Plated vs. Bare Steel Cylinders
Cylinder bore material significantly impacts honing parameters:
Hard Chrome-Plated Bores
- Surface hardness: 65-70 HRC (Rockwell C scale)
- Ra target: 0.15-0.25 μm typical
- Honing requirements: Diamond or CBN abrasives mandatory
- Advantages: Superior wear resistance, corrosion protection, reduced maintenance
- Applications: Mobile equipment, harsh environments, long service intervals
Bare Steel Bores (Non-plated)
- Surface hardness: 45-55 HRC after heat treatment
- Ra target: 0.20-0.40 μm typical
- Honing requirements: Aluminum oxide or silicon carbide stones
- Advantages: Lower initial cost, easier repair/refinishing
- Applications: Lower-pressure industrial cylinders, cost-sensitive applications
Chrome-plated cylinders require specialized honing equipment capable of processing hard materials. Krishna Enterprise SP-625 and SP-850 series machines accommodate both material types through appropriate abrasive selection and process parameter adjustment.
The Crosshatch Pattern: Angle, Depth, and Oil Retention
What is the Proper Crosshatch Angle for Hydraulic Cylinders?
The crosshatch pattern—the distinctive diagonal pattern visible on honed surfaces—results from the combination of rotational and reciprocating motion during honing. This pattern is not merely aesthetic; it performs critical functions in hydraulic cylinder operation.
Standard Crosshatch Specification: 45° ±3°
This angle represents the optimal balance between oil retention, seal wear, and machining efficiency for most hydraulic applications. Here’s why:
Angles Below 35° (Too Shallow):
- Insufficient oil retention capacity
- Seals wear rapidly from inadequate lubrication
- High friction generates excessive heat
- Premature seal failure common
Angles 40-50° (Optimal Range):
- Maximum oil retention in crosshatch valleys
- Excellent seal conformance and seating
- Balanced seal wear patterns
- Industry-standard recommendation
Angles Above 55° (Too Steep):
- Reduced oil retention effectiveness
- Seals may not track properly in grooves
- Uneven wear patterns develop
- Less common in hydraulic applications
Controlling Crosshatch Angle During Honing
Crosshatch angle is determined by the relationship between rotational speed (RPM) and reciprocating speed (strokes per minute):
Formula: Crosshatch Angle = arctan (Circumferential Speed / Reciprocating Speed)
Modern CNC honing machines maintain precise crosshatch control through programmable speed relationships. Operators specify the desired angle, and the control system automatically calculates and maintains optimal speeds throughout the honing cycle.
Manual Honing Machines: Require operator adjustment of speed settings and monitoring of actual pattern. Experienced operators verify angle using crosshatch measurement gauges.
CNC Honing Systems: Automatically maintain programmed crosshatch angle with ±1° accuracy regardless of bore diameter or length variations.
Crosshatch Depth and Oil Retention
Crosshatch depth—the vertical measurement from peak to valley in the surface texture—directly affects oil retention capacity:
Shallow Crosshatch (0.5-1.0 μm depth):
- Limited oil retention
- Suitable for low-pressure, slow-cycling applications
- Requires frequent seal replacement
Medium Crosshatch (1.5-2.5 μm depth):
- Optimal for most hydraulic applications
- Excellent oil retention with good seal life
- Standard for mobile and industrial hydraulics
Deep Crosshatch (3.0+ μm depth):
- Excessive for hydraulic seals
- May prevent proper seal seating
- Can trap contaminants
- Generally avoided in modern practice
Achieving the correct crosshatch depth requires proper stone grit selection, expansion pressure, and cutting speed. Fine grit stones (280-400 grit) produce shallower patterns appropriate for standard hydraulic applications. Coarser stones may be used for initial roughing passes but should be followed by finishing with appropriate grit.
Material Considerations: Processing Different Cylinder Types
Honing Cast Iron Cylinder Liners
Cast iron remains popular for hydraulic cylinder liners due to excellent wear characteristics and natural lubricity:
Material Properties:
- Hardness: 200-250 BHN (Brinell Hardness Number)
- Graphite inclusions provide self-lubrication
- Good machinability with aluminum oxide abrasives
Honing Parameters:
- Abrasive: Aluminum oxide, 180-280 grit roughing, 400-600 grit finishing
- Surface speed: 30-45 m/min (100-150 ft/min)
- Expansion pressure: 2-4 bar (30-60 PSI)
- Coolant: Petroleum-based honing oil or synthetic with EP additives
- Target Ra: 0.25-0.40 μm
Challenges:
- Graphite smearing if cutting speed too slow
- Porosity requires careful inspection
- Cast iron dust contamination must be contained
Honing Hardened Steel Tubes
Heat-treated steel tubes (through-hardened or induction-hardened) offer superior strength:
Material Properties:
- Hardness: 45-55 HRC after heat treatment
- Uniform hardness throughout wall thickness
- Requires more aggressive abrasives than cast iron
Honing Parameters:
- Abrasive: Silicon carbide or ceramic, 120-220 grit roughing, 280-400 grit finishing
- Surface speed: 25-35 m/min (80-120 ft/min)
- Expansion pressure: 3-5 bar (45-75 PSI)
- Coolant: Synthetic honing fluid with high lubricity
- Target Ra: 0.20-0.35 μm
Best Practices:
- Stress-relieve after heat treatment before honing
- Monitor for heat discoloration indicating overheating
- Allow cooldown between passes on long cylinders
Honing Chrome-Plated Bores
Hard chrome plating provides exceptional wear resistance and corrosion protection:
Material Properties:
- Hardness: 65-70 HRC (extremely hard)
- Thin coating: 0.025-0.075mm (0.001-0.003″)
- Brittle material subject to cracking if mishandled
Honing Parameters:
- Abrasive: Diamond (preferred) or CBN (Cubic Boron Nitride), 180-320 grit
- Surface speed: 20-30 m/min (65-100 ft/min)
- Expansion pressure: 2-4 bar (30-60 PSI) – light pressure to avoid coating damage
- Coolant: Water-based synthetic with rust inhibitors
- Target Ra: 0.15-0.25 μm
Critical Considerations:
- Never use conventional abrasives – only diamond or CBN
- Insufficient stock removal may polish rather than cut
- Excessive pressure can cause chrome delamination
- Verify plating adhesion before honing
- Chrome dust is toxic – ventilation essential
For chrome-plated cylinder processing, Krishna Enterprise recommends SP-625 single-spindle CNC honing machines equipped with diamond tooling and precise pressure control to protect the valuable chrome coating while achieving required surface finish.
Honing Process Parameters: Speeds, Feeds, and Stone Selection
Rotational Speed (RPM)
Spindle rotation provides the cutting action in honing. Optimal speed depends on bore diameter and material:
Formula for Surface Speed: Surface Speed (m/min) = (π × Diameter (mm) × RPM) / 1000
Target Surface Speeds by Material:
- Cast iron: 30-45 m/min (100-150 ft/min)
- Steel (unhardened): 25-40 m/min (80-130 ft/min)
- Hardened steel: 25-35 m/min (80-120 ft/min)
- Chrome plate: 20-30 m/min (65-100 ft/min)
Example Calculation: For 100mm bore in cast iron:
- Target: 35 m/min surface speed
- RPM = (35 × 1000) / (π × 100) = 111 RPM
Modern CNC honing machines automatically calculate and maintain optimal RPM based on programmed bore diameter and material parameters.
Reciprocating Speed (Strokes Per Minute)
Reciprocation creates the characteristic crosshatch pattern and ensures even material removal along the bore length:
Typical Reciprocation Rates:
- Short cylinders (<500mm): 15-25 strokes/min
- Medium cylinders (500-1500mm): 10-18 strokes/min
- Long cylinders (>1500mm): 8-15 strokes/min
Stroke Overtravel:
- Tool must extend 1/3 of stone length beyond bore ends
- Ensures complete finishing to bore edges
- Prevents bell-mouth formation at bore ends
Expansion Pressure and Material Removal Rates
Stone expansion pressure determines cutting force and material removal rate:
Roughing Operations:
- Pressure: 3-6 bar (45-90 PSI)
- Material removal: 0.05-0.15mm (0.002-0.006″) per pass
- Purpose: Remove boring tool marks, correct geometry
Semifinishing Operations:
- Pressure: 2-4 bar (30-60 PSI)
- Material removal: 0.02-0.05mm (0.0008-0.002″) per pass
- Purpose: Refine surface, establish crosshatch
Finishing Operations:
- Pressure: 1-3 bar (15-45 PSI)
- Material removal: 0.005-0.015mm (0.0002-0.0006″) per pass
- Purpose: Achieve final Ra and dimensional tolerance
Servo-Hydraulic Expansion Systems: Modern CNC honing machines employ servo-hydraulic expansion with 0.001mm resolution, enabling precise control throughout the honing cycle. The control system can program different pressures for roughing and finishing within a single automated cycle.
Abrasive Stone Selection
Stone selection impacts surface finish, material removal rate, and tool life:
Aluminum Oxide (Conventional):
- Materials: Cast iron, soft steel, aluminum
- Grits: 80-600
- Cost: Low
- Applications: General-purpose, non-ferrous
Silicon Carbide:
- Materials: Cast iron, hardened steel (up to 55 HRC)
- Grits: 120-600
- Cost: Moderate
- Applications: Harder materials than aluminum oxide can handle
CBN (Cubic Boron Nitride):
- Materials: Hardened steel (50-65 HRC), cast iron
- Grits: 100-400
- Cost: High (but exceptional tool life)
- Applications: High-volume production, hardened materials
Diamond:
- Materials: Chrome plate, carbide, ceramics, hardened steel
- Grits: 100-600
- Cost: Highest (but longest tool life)
- Applications: Ultra-hard materials, precision finishing
Grit Selection Guide:
- Coarse (80-150 grit): Rapid stock removal, roughing only
- Medium (180-280 grit): General-purpose roughing and semifinishing
- Fine (320-400 grit): Standard finishing for Ra 0.2-0.4 μm
- Very Fine (500-600 grit): Ultra-smooth finishing for Ra <0.2 μm
Coolant Selection and Management
Honing fluid serves multiple critical functions:
Functions:
- Lubrication: Reduces friction between abrasive and workpiece
- Cooling: Removes heat generated during cutting
- Flushing: Carries away chips and prevents loading of abrasive
- Corrosion protection: Protects cylinder bore during processing
Coolant Types:
Petroleum-Based Honing Oils:
- Traditional choice for cast iron and steel
- Excellent lubricity and corrosion protection
- Requires disposal considerations
- Typical mix: Straight cutting oil or 5-10% emulsifiable oil in water
Synthetic Honing Fluids:
- Modern alternative with environmental advantages
- Water-based with synthetic lubricants and corrosion inhibitors
- Better cooling capacity than straight oils
- Easier cleanup and disposal
- Required for chrome-plated cylinders
Coolant Flow Rate:
- Minimum: 60-80 liters/min (15-20 GPM) for cylinders up to 200mm diameter
- Large cylinders: 100-150 liters/min (25-40 GPM) for 400mm+ diameters
- Flood application ensures complete chip evacuation
Coolant Maintenance:
- Monitor concentration (refractometer for emulsions)
- Filtration: 25-50 micron recommended
- Temperature control: 18-25°C (65-77°F) optimal
- Regular testing for bacterial growth (synthetic fluids)
- Change per manufacturer recommendations
Selecting the Right Honing Machine for Hydraulic Cylinder Applications
Single-Spindle CNC Honing Machines
Single-spindle machines offer maximum flexibility for cylinder manufacturers and repair shops processing diverse bore sizes:
Ideal Applications:
- Job shops handling varied cylinder sizes
- Prototype and low-volume production
- Cylinder repair and reconditioning operations
- Bore ranges from 40mm to 850mm+
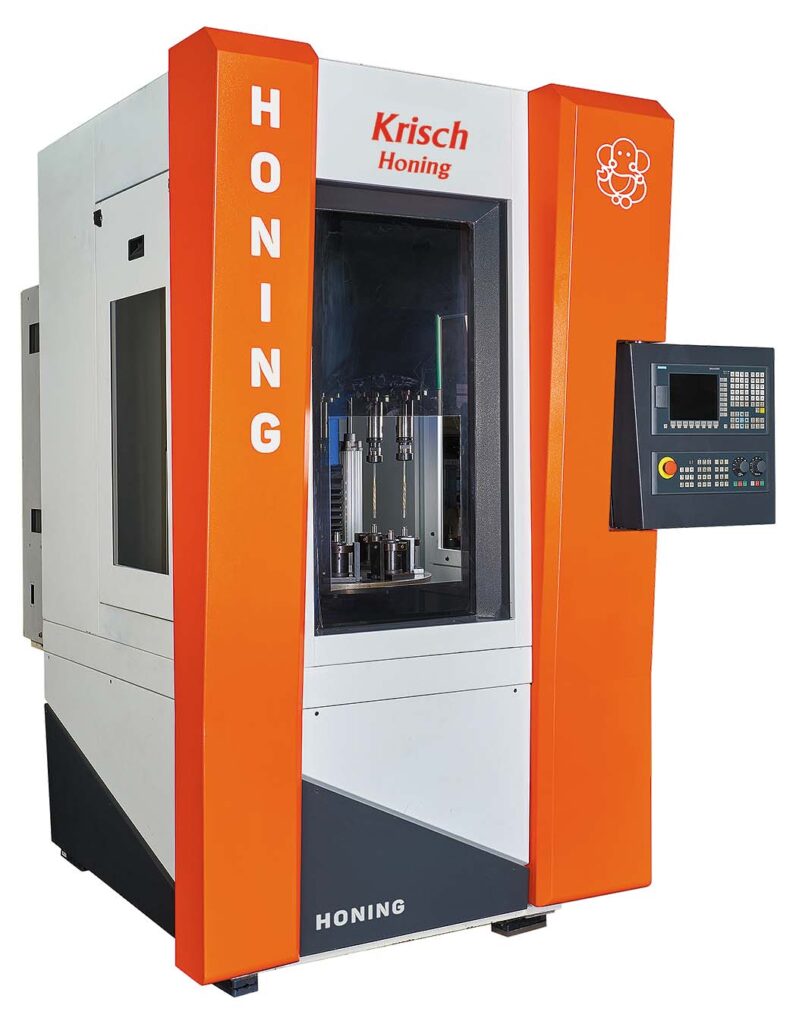
Krishna Enterprise SP-625: The Hydraulic Cylinder Specialist
The SP-625 single-spindle CNC honing machine is specifically engineered for hydraulic cylinder applications:
Key Specifications:
- Bore diameter range: 40-625mm (1.6″-24.6″)
- Maximum stroke length: 2,500mm (98″)
- Spindle motor: 11 kW variable frequency drive
- Expansion system: Servo-hydraulic, 0.001mm resolution
- Control: Siemens 828D or Fanuc 0i-MF CNC
- Accuracy: ±0.004mm cylindricity over full bore length
Why SP-625 Excels for Hydraulic Cylinders:
1. Servo-Hydraulic Expansion The precision servo-hydraulic system maintains exact stone pressure throughout the cycle, automatically compensating for tool wear. This ensures consistent crosshatch pattern and surface finish from first cylinder to last in a production run.
2. Programmable Crosshatch Control CNC system calculates and maintains precise 45° ±1° crosshatch angle automatically. Operator programs desired angle; machine handles speed relationships regardless of bore diameter changes.
3. Real-Time Process Monitoring Control system displays expansion position, cutting force, and dimensional trends. Adaptive control automatically adjusts parameters if deviations occur, preventing scrap.
4. Multi-Stage Programming Single program executes roughing, semifinishing, and finishing operations automatically. Different stone grits, pressures, and speeds for each stage ensure optimal results with minimal operator intervention.
Production Example: A mobile equipment cylinder manufacturer processes 80-120mm bore cylinders with 600-1200mm lengths on an SP-625. Typical cycle time: 6-8 minutes including loading. Production capacity: 60-80 cylinders per 8-hour shift with one operator.
Vertical Honing Machines for Large-Diameter Cylinders
Large construction equipment and industrial cylinders benefit from vertical configuration:
Advantages of Vertical Honing:
- Gravity assists chip removal from bore
- Easier loading/unloading of heavy cylinders
- Reduced floor space vs. horizontal machines of equivalent capacity
- Better access for operator during setup
Krishna Enterprise VH-1000 Series
The VH-1000 vertical CNC honing machine handles large construction equipment and industrial press cylinders:
Key Specifications:
- Bore diameter range: 200-1000mm (8″-40″)
- Maximum stroke length: 3,000mm (118″)
- Spindle motor: 15 kW variable frequency drive
- Table load capacity: 2,000 kg (4,400 lbs)
- Hydraulic table height adjustment: Programmable positioning
Ideal For:
- Excavator boom/arm/bucket cylinders
- Large industrial press cylinders
- Marine and power generation cylinders
- Heavy equipment cylinder repair shops
CNC Control Benefits for Consistent Results
Modern CNC honing machines deliver advantages impossible with manual equipment:
Consistency:
- Identical results cylinder after cylinder
- Eliminates operator skill variations
- Ensures specification compliance every cycle
Documentation:
- Automatic data logging of all process parameters
- Quality reports with dimensional measurements
- Traceability for ISO/TS compliance
- Statistical process control (SPC) data export
Productivity:
- Automatic tool wear compensation
- Multi-stage operations without manual adjustment
- Reduced setup time through program storage
- Fewer rejected parts from human error
For manufacturers processing 20+ cylinders daily, CNC honing machines typically show ROI within 12-18 months through reduced labor, improved quality, and eliminated rework costs.
Explore Krishna Enterprise’s complete range of CNC honing solutions to find the optimal configuration for your hydraulic cylinder applications.
Troubleshooting Common Hydraulic Cylinder Honing Issues
Problem: Premature Seal Wear
Symptoms:
- Seals require replacement within months instead of years
- Visible wear pattern on seal surface
- Increased leakage over time
Possible Causes & Solutions:
| Cause | Verification Method | Solution |
|---|---|---|
| Crosshatch angle incorrect (>55° or <35°) | Measure with crosshatch gauge | Adjust RPM to reciprocating speed ratio to achieve 45° ±3° |
| Surface finish too rough (Ra >0.5 μm) | Profilometer measurement | Use finer grit stones (400-600 grit) for finishing pass |
| Surface finish too smooth (Ra <0.1 μm) | Profilometer measurement | Reduce final grit size or increase stone pressure slightly |
| Insufficient crosshatch depth | Microscopic examination | Increase stone aggressiveness or cutting pressure |
Problem: Hydraulic Fluid Leakage Past Seals
Symptoms:
- Visible fluid seepage at rod seals
- System requires frequent fluid top-up
- External contamination and environmental concerns
Possible Causes & Solutions:
| Cause | Verification Method | Solution |
|---|---|---|
| Poor cylindricity (>0.01mm) | Bore gauge or CMM | Verify honing machine geometry, check tool expansion system |
| Bell mouth at bore ends | Indicator measurement at ends vs. center | Ensure proper stroke overtravel (1/3 stone length minimum) |
| Spiral pattern instead of crosshatch | Visual inspection | Adjust reciprocating speed, verify stroke length consistency |
| Contamination embedded in surface | Visual/microscopic exam | Improve coolant filtration, clean bore thoroughly before sealing |
Problem: Inconsistent Surface Finish Along Bore Length
Symptoms:
- Rough finish at one end, smooth at other
- Ra measurements vary by >20% along length
- Visible finish variation
Possible Causes & Solutions:
| Cause | Verification Method | Solution |
|---|---|---|
| Inadequate reciprocation speed | Observe stroke rate | Increase strokes per minute for more even material removal |
| Tool deflection in long bores | Straightness measurement | Use larger diameter tooling, reduce stroke speed, add guide bushings |
| Coolant flow insufficient | Flow meter check | Increase coolant flow rate, verify nozzle positioning |
| Stone loading (glazing) | Visual inspection of stones | Dress stones, adjust coolant concentration, reduce pressure |
Problem: Dimensional Out-of-Tolerance
Symptoms:
- Bore diameter outside specification
- High/low readings at different points
- Rejection during final inspection
Possible Causes & Solutions:
| Cause | Verification Method | Solution |
|---|---|---|
| Tool wear not compensated | Measure first part vs. last part in run | Enable automatic tool wear compensation in CNC program |
| Thermal growth during processing | Temperature monitoring | Allow thermal stabilization, control coolant temperature |
| Excessive material removal | Check programmed stock removal | Reduce number of passes or expansion pressure |
| Measurement error | Calibrate measurement equipment | Verify bore gauge calibration, measure at proper temperature |
Problem: Taper in Bore
Symptoms:
- Diameter larger at one end than other
- Seal binding or improper seating
- Piston rod misalignment
Possible Causes & Solutions:
| Cause | Verification Method | Solution |
|---|---|---|
| Uneven reciprocation (dwell at one end) | Observe reciprocation cycle | Adjust CNC stroke program, verify mechanical limits |
| Machine alignment issues | Level check, geometric verification | Perform machine alignment procedure, check guideways |
| Workpiece clamping distortion | Measure bore before and after unclamping | Reduce clamping force, use soft jaws, support cylinder mid-length |
| Stone configuration imbalanced | Measure stone expansion at ends | Ensure equal stone length, check for damaged stones |
Quality Control: Measuring and Verifying Honing Results
Surface Roughness Measurement
Profilometer Method (Most Accurate):
- Contact stylus measures actual surface profile
- Provides Ra, Rz, and other parameters
- Measures perpendicular to crosshatch pattern
- Portable units available for large cylinders
Comparison Gauges:
- Physical samples with known Ra values
- Visual and tactile comparison
- Less precise but useful for quick checks
- Common in repair shop environments
Measurement Procedure:
- Clean bore thoroughly – any contamination affects readings
- Take minimum 3 measurements at 120° positions
- Measure at multiple locations along bore length (entry, middle, exit)
- Average readings and note variation
- Document results for quality records
Crosshatch Angle Verification
Crosshatch Gauge Method:
- Specialized gauge with angle markings
- Place against honed surface
- Compare pattern to gauge marks
- Accurate to ±2-3°
Digital Photography Method:
- Photograph honed surface with scale reference
- Import to CAD or image analysis software
- Measure angle digitally
- More precise than visual gauges (±1° accuracy possible)
Dimensional Inspection
Bore Gauges (Most Common):
- Three-point contact measurement
- Available as dial indicators or digital readouts
- Measure at entry, middle, and exit of bore
- Record maximum, minimum, and average diameter
Coordinate Measuring Machine (CMM):
- Highest accuracy for cylindricity and straightness
- Generates complete bore profile
- Expensive but ideal for critical cylinders
- Documents compliance with tight tolerances
Inspection Frequency:
- First cylinder: 100% dimensional verification
- Production run: Check every 10th cylinder minimum
- After tool changes: Verify first part
- If process disruption: Immediate verification
Documentation for Quality Management Systems
ISO 9001 and IATF 16949 certified manufacturers require documented evidence of process control:
Required Documentation:
- Honing process specification (parameters, tooling, coolant)
- Measurement procedures and calibrated equipment records
- Dimensional inspection results with date/time/operator
- Surface finish measurements (Ra values, crosshatch angles)
- Statistical process control (SPC) charts showing trends
- Corrective action records for out-of-spec conditions
Modern CNC honing machines with data logging automatically capture process parameters, eliminating manual record-keeping and ensuring complete traceability.
Conclusion: Achieving Optimal Hydraulic Cylinder Performance Through Precision Honing
Hydraulic cylinder honing represents far more than a finishing operation—it’s a precision manufacturing process that directly determines system reliability, efficiency, and service life. Proper bore finishing with controlled crosshatch patterns, accurate surface roughness, and precise geometry creates the foundation for effective sealing under the demanding conditions hydraulic systems face daily.
The technical requirements are specific and non-negotiable:
- Surface finish: Ra 0.2-0.4 μm for standard applications
- Crosshatch angle: 45° ±3° for optimal oil retention and seal life
- Cylindricity: ±0.005mm maximum variation over bore length
- Straightness: ±0.01mm per 100mm to prevent seal binding
Achieving these specifications consistently requires more than manual skill—it demands precision equipment with proper controls, appropriate tooling, and verified process parameters. Whether you’re manufacturing thousands of cylinders annually or reconditioning equipment cylinders in a repair shop, the quality of your honing equipment directly impacts your final product quality and operational costs.
Selecting the Right Honing Solution
For manufacturers and repair shops processing hydraulic cylinders, equipment selection should consider:
Bore diameter range: Ensure machine capacity covers your smallest and largest cylinders with some margin for future growth. Krishna Enterprise’s SP-625 handles 40-625mm bore range, covering most mobile equipment and industrial cylinders.
Stroke length capacity: Verify adequate stroke to process your longest cylinders with proper tool overtravel. Construction equipment boom cylinders may require 2,500-3,000mm stroke capability.
Control system sophistication: CNC control eliminates operator variability and provides consistency impossible with manual machines. Programmable crosshatch, automatic tool compensation, and process monitoring ensure reliable results.
Expansion system precision: Servo-hydraulic expansion with micron-level resolution delivers the surface finish consistency that seal manufacturers specify and hydraulic system designers demand.
For large-diameter cylinders common in construction equipment and industrial presses, vertical honing machine configurations offer handling advantages and space efficiency.
Engineering Support for Your Application
Krishna Enterprise provides comprehensive application engineering support for hydraulic cylinder honing:
Process Development Services:
- Sample cylinder testing and process parameter development
- Surface finish verification and crosshatch analysis
- Tool selection and configuration recommendations
- Quality control procedure establishment
- Operator training and process documentation
Equipment Selection Consultation:
- Analysis of your bore diameter and length range requirements
- Production volume assessment and capacity planning
- Configuration recommendations (single-spindle vs. vertical)
- Tooling and accessory requirements
- Installation and commissioning support
Whether you’re establishing new cylinder manufacturing capability or upgrading existing honing operations, our engineering team brings decades of experience in hydraulic cylinder applications across construction equipment, mobile hydraulics, and industrial machinery sectors.
Ready to Discuss Your Hydraulic Cylinder Honing Requirements?
Achieving consistent, reliable hydraulic cylinder bore finishing requires the right combination of equipment capability, process expertise, and technical support. Krishna Enterprise has partnered with cylinder manufacturers and repair facilities worldwide to implement precision honing solutions that deliver measurable results in seal life, system reliability, and production efficiency.
Take the Next Step:
Contact Our Engineering Team
Discuss your specific bore diameter range, production volumes, and quality requirements with our application engineers.
Schedule Technical Consultation →
Explore Honing Equipment Solutions
Review complete specifications for Krishna Enterprise CNC honing machines engineered for hydraulic cylinder applications:
- SP-625 Single-Spindle CNC Honing Machine – Versatile solution for 40-625mm bore range
- VH-1000 Vertical CNC Honing Machine – Specialized for large construction equipment cylinders
- Complete Honing Machines Range – Full portfolio of precision honing solutions
📚 Learn More About Honing Technology
For comprehensive coverage of honing processes, equipment types, and industry applications, see our Complete Guide to Honing Machines and Manufacturing Technology.
About Krishna Enterprise
Founded in 2015, Krishna Enterprise manufactures precision CNC honing machines serving automotive, aerospace, hydraulics, and industrial manufacturing sectors worldwide. Our ISO 9001:2015 certified facility combines advanced manufacturing technology with application engineering expertise to deliver honing solutions that meet the demanding requirements of global manufacturers.
Our equipment operates in facilities of leading manufacturers including Godrej and Bosch, producing millions of precision components annually. From prototyp development to high-volume production, Krishna Enterprise provides the technology, expertise, and support that manufacturing excellence demands.
For more information about hydraulic cylinder honing equipment and process support, contact Krishna Enterprise at info@krischoning.com
Related Articles:
Founded in 1994 by Mr. Ajeet Samani, Krishna Enterprise began as a small workshop with a vision to provide precision honing solutions to the manufacturing industry. Over the past two decades, we have grown into a respected name in the honing machine manufacturing sector, serving clients across India and internationally.